
Introduction: a question that starts the comparison
Have you ever wondered why two shops with similar budgets end up with such different parts and uptime? Recent industry surveys show variability in tolerance, cycle time, and service response across suppliers—data that matters when you invest in heavy kit. In my experience evaluating suppliers, I’ve found that 5 axis CNC machining center manufacturers vary widely in how they define quality, support, and real-world throughput.
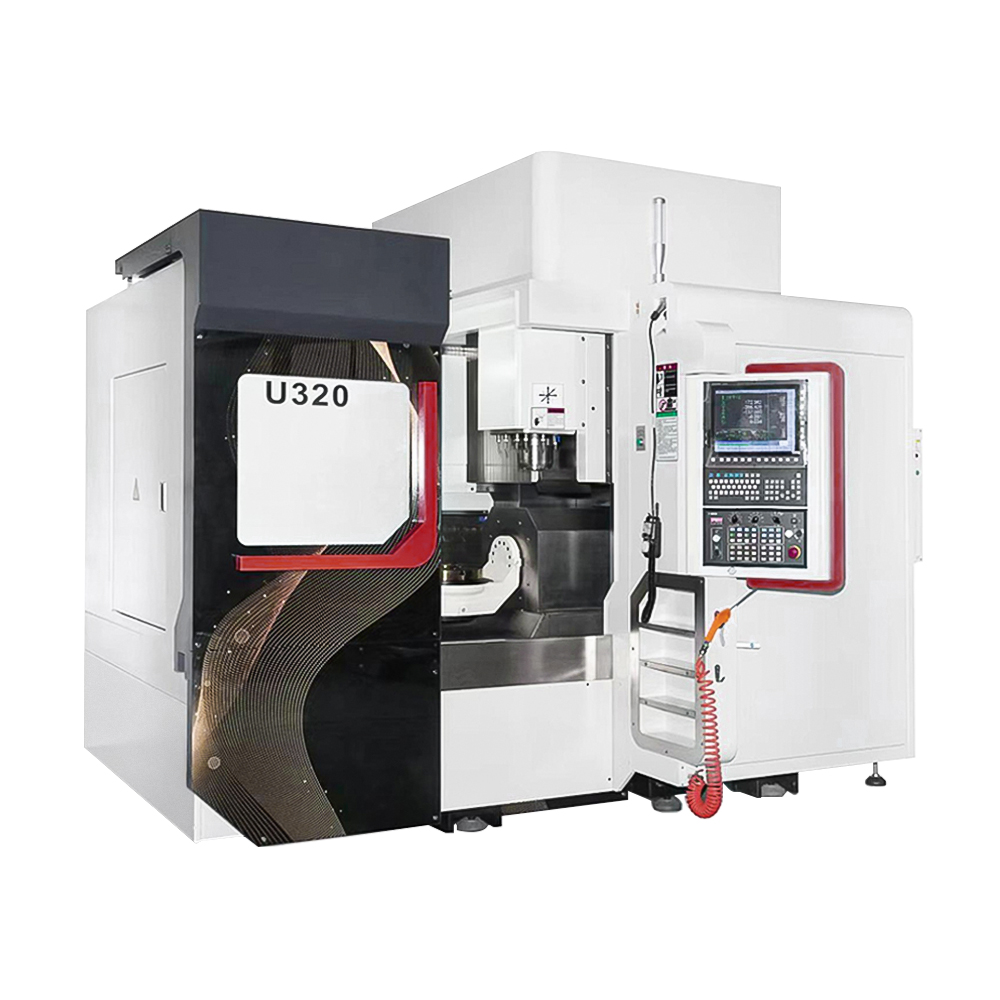
Picture a mid-size aerospace shop running prototypes, a job shop taking on high-mix small runs, and a toolroom upgrading to handle complex geometries—each needs different guarantees (lead times, training, retrofit paths). I use these scenarios to test vendors. Which metrics should you ask for first? How do you weigh spindle power versus true position accuracy when your parts demand five-micron precision? These are the questions I’ll examine next, and I’ll share practical ways to compare suppliers so you don’t end up buying service headaches along with a machine.
Part 2 — Where traditional solutions fail: a technical look
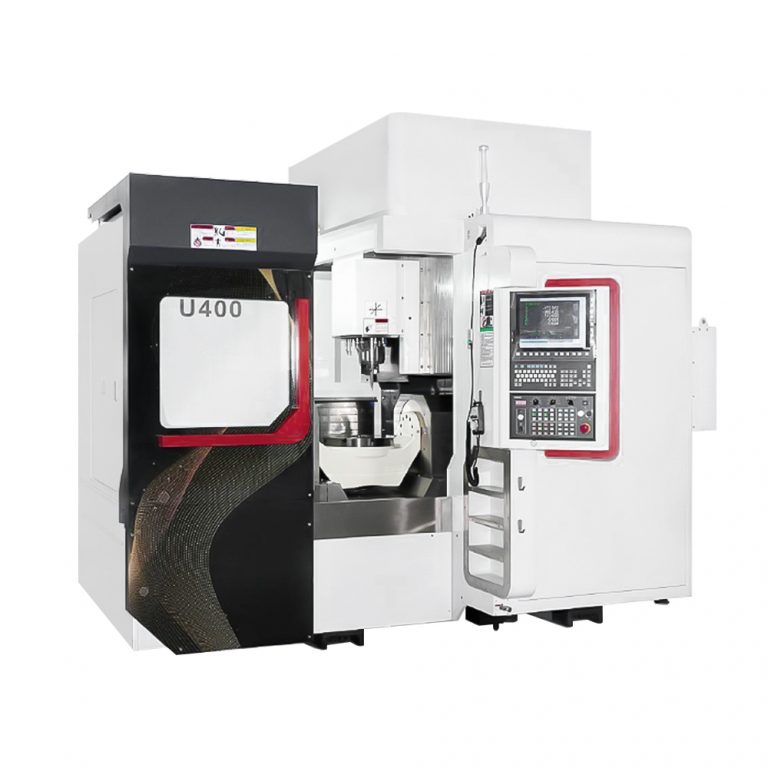
simultaneous 5-axis machining center platforms promise flexibility, but many standard offers gloss over the mechanics that make them reliable. I’ll be technical here because the flaws are mechanical and software-deep: poor kinematic calibration, imprecise toolpath interpolation, and weak servo drives all chip away at accuracy. When vendors tout catalog spindle speeds, they often omit how spindle torque and thermal drift affect long-run accuracy.
What exactly fails?
Look, it’s simpler than you think: tolerance loss usually comes from a chain of small issues. Backlash compensation might be set loosely, encoder feedback may lack resolution, and axis coupling gets worse under load—so your G-code looks perfect, but the finished geometry doesn’t match. I’ve seen fixtures redesigned repeatedly simply because manufacturers ignored thermal growth and power converter behavior during long cycles. The result? Boards, panels, and inspection logs filled with workarounds rather than design fixes — funny how that works, right?
Part 3 — Future outlook and practical comparisons
Now I shift forward. I want to talk about what’s coming and what to demand. Modern five axis cnc machine control blends better real-time interpolation, predictive maintenance hooks, and improved kinematic models. Vendors who invest in sensor fusion—integrating spindle torque sensing, axis encoder diagnostics, and thermal probes—give you a practical edge. In one case I tracked, adding closed-loop spindle monitoring cut scrap by 18% within three months. Those gains aren’t marketing fluff; they’re measurable.
What’s Next?
If you’re comparing offers, focus on three concrete evaluation metrics: accuracy under load (measured at part level), mean time to repair with certified parts, and effective software support for toolpath optimization. I recommend test-cuts that mimic your worst-case jobs and insist on documented kinematic calibration routines. Also weigh retrofitability: can the controller accept future encoder upgrades or new servo tuning algorithms? — and yes, timing matters.
To wrap up: I’ve learned to judge suppliers by evidence, not promises. Ask for part-level data, insist on transparency about thermal behavior and service logistics, and prioritize systems with clear sensor and control roadmaps. Those three metrics will save you money and downtime. For a dependable partner, consider talking directly with specialists like Leichman—they tend to provide the documentation and testing I look for, which makes my life easier and, honestly, helps yours too.