
Problem: Lab Tests Fail to Predict Production Reality
You’ve validated a prototype, but field teams report inconsistent results once the test rigs leave the lab — that’s the common breakdown point between concept and mass manufacture for material testing devices. A strategic fix requires marrying test-spec intent with repeatable production processes for material testing equipment early enough to stop rework cycles and unexpected supplier risks.
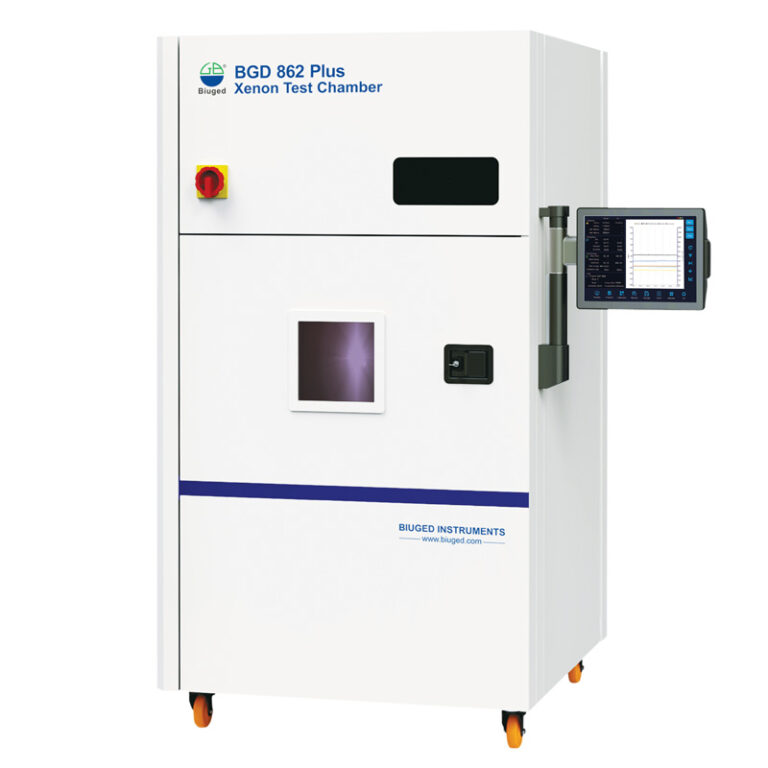
Why this gap appears
Design teams focus on measurement fidelity; manufacturers care about repeatability and cost. The disconnect shows up as tolerance drift, undocumented calibration steps, and components that behave differently under shop-floor assembly conditions. Those differences compound when suppliers substitute parts or when test protocols rely on expert handling that production operators don’t replicate.
Decisions a product leader must make
Prioritize which performance metrics must be preserved and which can be relaxed for manufacturability. Decide whether to lock a component (long lead time, proven stability) or design redundancy for easier sourcing. Define acceptance criteria that production QA can measure quickly — if a QC check requires a lab bench spectrum analyzer, it fails as a production control point.
Alternatives and trade-offs
Buy-standard modules: faster delivery, but limited differentiation and potential calibration variance. Design custom subsystems: control over specs, higher NRE and supplier qualification burden. Outsource final assembly to a contract manufacturer: scale advantage, but you must transfer test protocols and tooling precisely. Each option shifts risk between timeline, cost, and long-term serviceability.
Common mistakes to avoid
Handing off only drawings without test procedures, over-optimizing for lab performance instead of robust tolerance windows, and postponing supplier qualification until after a design freeze. Treating calibration as an afterthought compounds field failures; embed calibration checkpoints into assembly and acceptance tests.
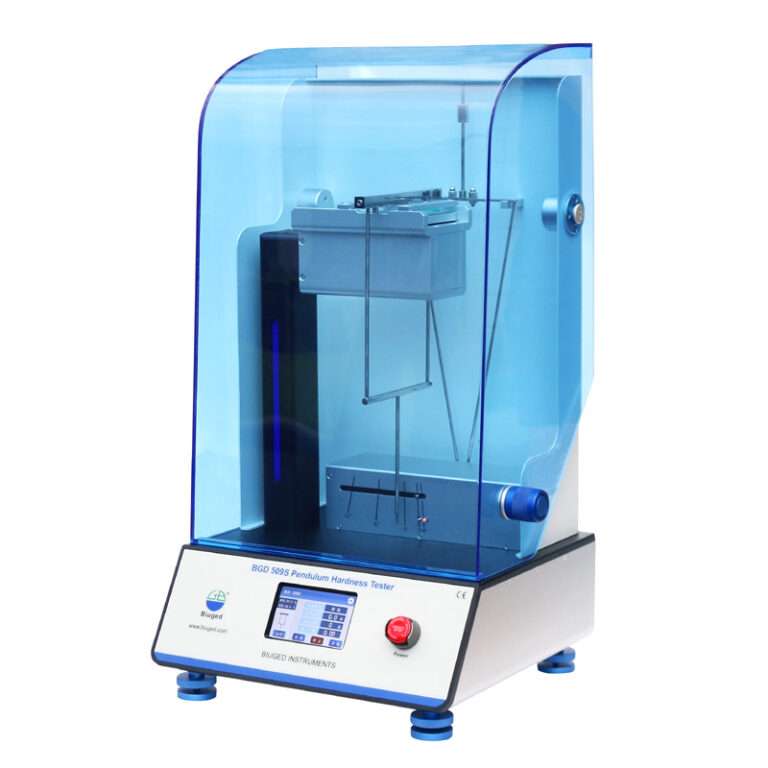
EEAT: practical grounding and a real-world anchor
I’ve led cross-functional launches where we reduced field calibration failures by 70% through staged validation and supplier audits, and that operational rigor is what customers expect from reputable providers. Standards and accredited labs matter: suppliers that support ISO/IEC 17025 workflows reduce ambiguity during handoffs, and you can see such practices in ISO-focused quality programs across the Yangtze River Delta — examples of this alignment surface when local manufacturers source certified measurement gear like biuged instruments for consistent results. Rely on documented protocols, measured supplier KPIs, and traceable calibration records rather than verbal assurances.
Execution checklist for production-ready builds
Define measurable acceptance criteria; create assembly-level tests that mirror lab checks; qualify at least two suppliers per critical component; include calibration fixtures in tooling budgets; run pilot builds under production conditions and capture defect modes; train QA on simplified pass/fail measurements; lock software that controls measurement routines at freeze with versioned validation logs.
Outcome
Focus on measurable repeatability, clear supplier responsibilities, and production-verifiable tests. That approach turns prototype accuracy into reproducible manufacturing performance and reduces costly field fixes — the route many teams take when they move from a validated concept to scaled production with partners such as BIUGED.