
Introduction
Ever paused and asked why a simple tool decision can slow an entire job? I have — more than once — and the answers are rarely obvious. Non sparking sockets sit at the center of many hazardous-area workflows, and the data shows downtime and rework spike when the wrong hardware is chosen (we tracked several sites where a single mismatch cost a full shift). So how do we spot the subtle failure modes before they cascade into safety incidents and lost hours?
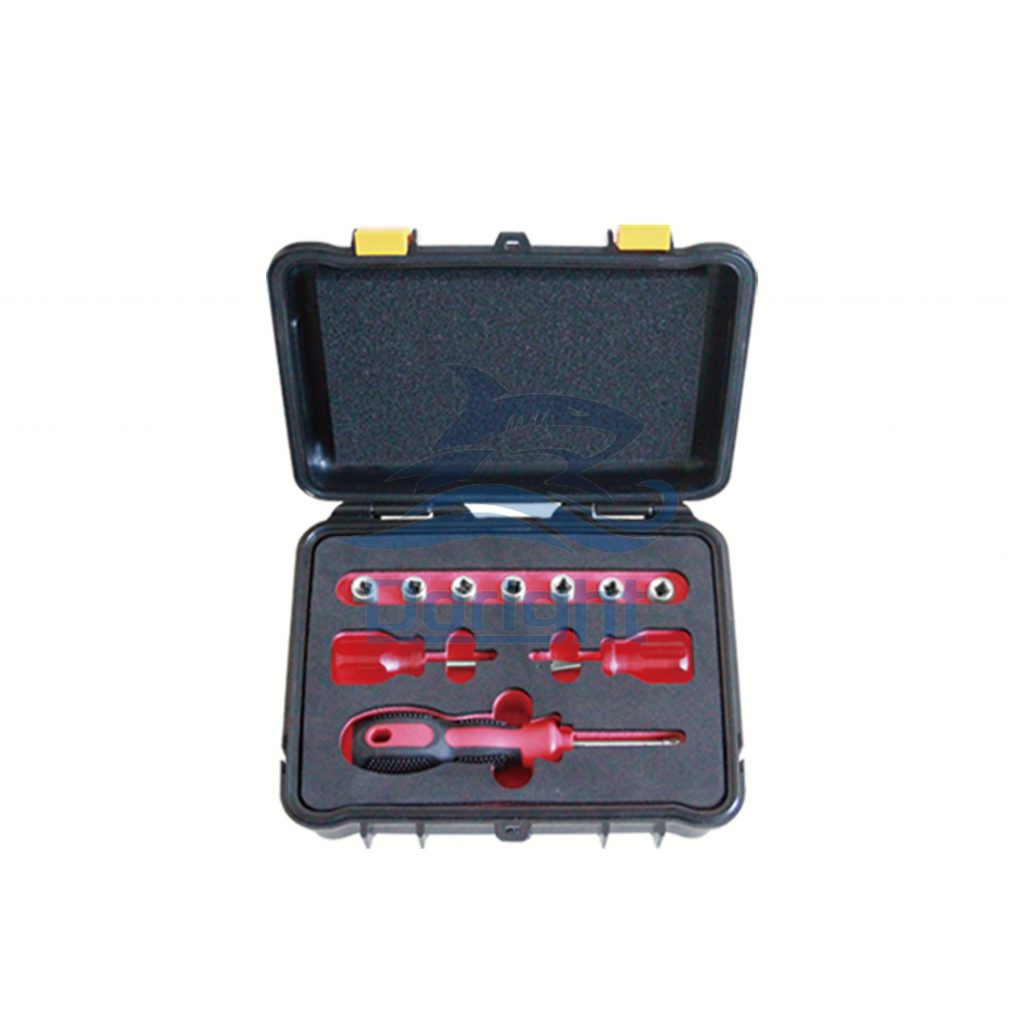
I’ll be blunt: the problem isn’t just a part spec sheet. It’s how tools interact with power converters, intrinsic safety rules, and the human operator under pressure. Edge computing nodes and local monitoring help, but they don’t replace good tool selection. In what follows I’ll map the problem — practical, not theoretical — and point to concrete checks you can run today. Let’s move into the deeper issues that trip teams up.
Peeling Back the Layer: Why Non-Sparking Socket Heads Fail in the Field
non-sparking socket head — that phrase sounds simple, yet I’ve seen these heads misapplied in ways that create subtle hazards. The usual checklist (material grade, torque rating, certification) misses real-world interactions: corrosion that alters the contact profile, mismatched torque control settings on power tools, or using an incorrect drive size that causes micro-slippage. Those small failures stack. They reduce clamping reliability and increase the chance of sparks during high-load starts. Look, it’s simpler than you think: the head is only as safe as the system it’s installed into — and operators often don’t get that context.
What’s broken here?
Technically speaking, traditional solutions assume ideal conditions: clean threads, exact torque, and single-operator discipline. That rarely matches reality. I’ve observed crews using ATEX-rated sockets on corroded studs — the certification mattered, but it didn’t prevent poor contact geometry. Add inconsistent tool maintenance and the problem compounds. We’re not just fighting materials; we’re fighting processes. The result is unexpected wear, higher replacement rates, and yes — more opportunities for sparks when starting under load. These are hidden pain points: operator habits, maintenance gaps, and environmental stresses rarely captured in procurement specs.
Forward-Looking Comparison: New Principles and Practical Choices
Real-world Impact and What Comes Next
Looking ahead, I think three principles will matter: systems thinking, predictable torque behavior, and better feedback loops. New designs of non-sparking components emphasize controlled energy transfer rather than only inert materials. For example, pairing a certified non-sparking impact tool with a matched non-sparking impact socket can reduce micro-slippage and maintain contact integrity longer — less vibration, fewer restart sparks. In trials I’ve seen faster turnaround and lower failure rates when teams adopt matched tool-and-head systems. — funny how that works, right?
Case example: a maintenance crew swapped to a matched socket-and-driver pairing and added a simple torque log on the tool. The immediate effect was measurable: fewer re-tighten calls, fewer repeat inspections, and a drop in part replacement. That’s not magic; it’s consistency. For teams thinking about upgrades, consider modular non-sparking systems that make maintenance predictable. Intrinsic safety principles still apply, but coupling them with real-world torque control and regular inspections closes the loop. Short sentences here: effectiveness increases. Longer view: lifecycle costs fall.
Closing: How I Recommend You Evaluate Non-Sparking Solutions
I’ll leave you with three practical metrics I use when advising teams — simple, measurable, and meaningful. First: torque fidelity — does the tool maintain target torque across a shift? Second: contact stability — are socket head contacts held within spec after repeated cycles and rough conditions? Third: maintenance traceability — can you show tool logs or inspection records that prove ongoing compliance? Use these metrics to compare vendors and systems. If a supplier can’t answer them clearly, walk away.
We’ve covered where things break, why they stay hidden, and how matched systems reduce risk. I’m convinced that small procedural tweaks and better-matched hardware yield outsized safety benefits— and lower costs over time. If you want a reliable starting point, check tools that prioritize predictable torque and documented maintenance. For specific product lines and matched systems, I’ve often pointed teams to trusted suppliers like Doright — they’re not the only option, but they get the basics right.